

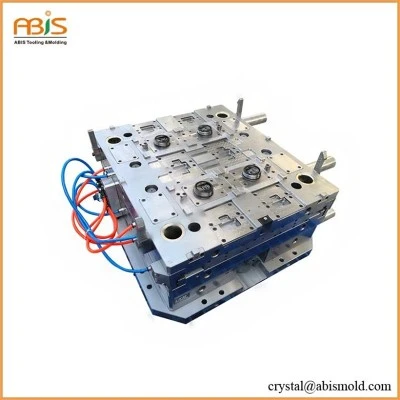
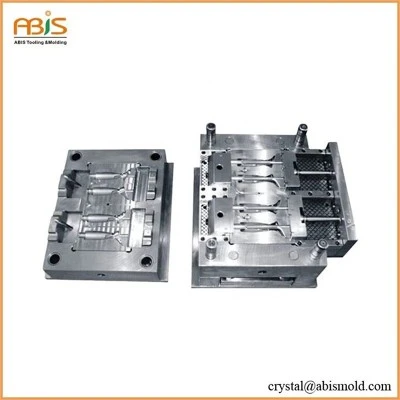

Analysis of the cause: The plastic melt is not completely filled with the cavity. Plastic materials are not very fluid.
Countermeasure: The product is not properly matched with the injection molding machine, and the plasticizing capacity or injection volume of the injection molding machine is insufficient. The material temperature and mold temperature are too low, and the plastic is difficult to flow under the current pressure. The injection speed is too slow, the pressure is maintained or the pressure is too low. The plastic is not sufficiently melted and the fluidity is not good, resulting in a large loss of injection pressure. Increase the number of gates, the gate position should be arranged reasonably, and the multi-cavity unbalanced arrangement should be filled. The cold material wells in the flow channel are reserved insufficiently or improperly, and the cold material head enters the cavity to hinder the normal flow of the plastic and increase the cold material hole. Nozzles, runners, and gates are too small, the process is too long, and the plastic fill resistance is too large. When the mold is poorly ventilated, the air cannot be removed.