
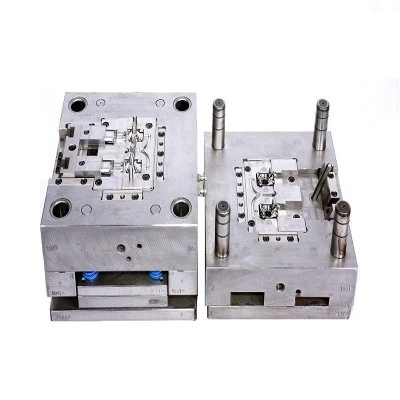
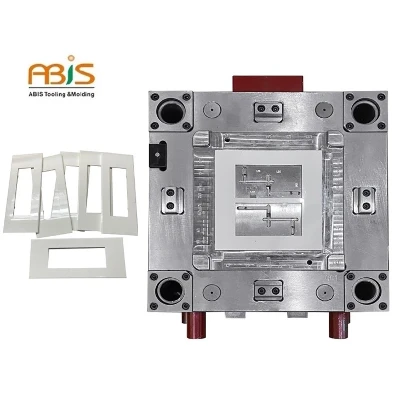


Shoot short or shrink the sample, if the whole parting surface run the edge, besides check the mold, also should check the machine.Open and close the mold manually, observe the pressure gauge first, confirm whether the die thickness adjustment meets the requirement of the clamping force, if not, adjust the thickness.Add that in the process of tuning machine, if there is a chief officer of the mold temperature changes, must confirm the clamping force again, because the mold thickness of heat bilges cold shrink or affect the change, but only the crankshaft type of the machine, direct pressure the machine won't appear this problem.
If the mold thickness is adjusted, the parting surface and the burr will need to be re-checked whether the tonnage of the machine is too small and the clamping force is not enough.One method is to refer to the data of model flow analysis.Another method is to use the empirical formula to follow up the projection area calculation of the vertical direction of the product.
If there is no problem with the locking force, the edge of the parting surface may be caused by the unbalance of the machine. In this case, the rough edges will be fixed on the same side of the machine, and the machine should be checked and adjusted.