
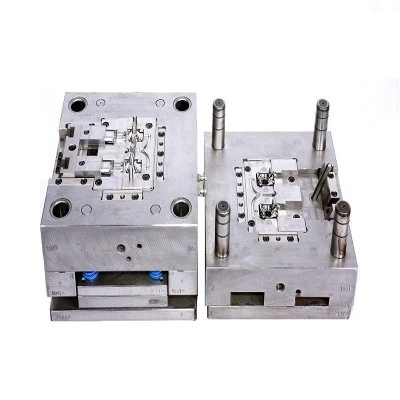
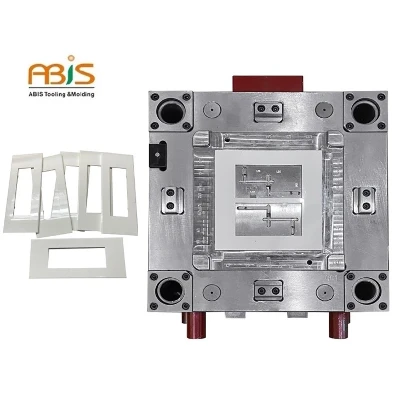

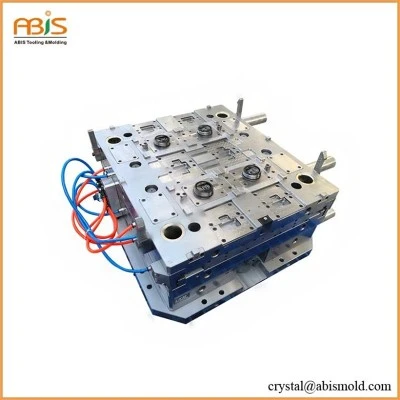
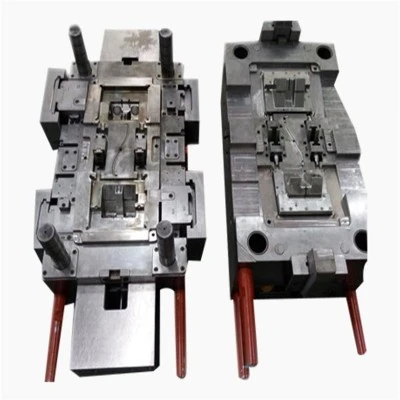
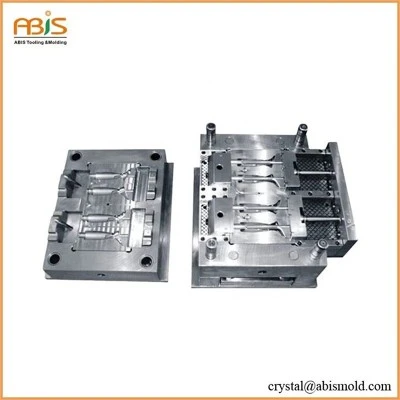

Forming dies are typically made by tool and die makers and put into production after mounting into a press. The die is a metal block that is used for forming materials like sheet metal and plastic. For the vacuum forming of plastic sheet only a single form is used, typically to form transparent plastic containers (called blister packs) for merchandise. Vacuum forming is considered a simple molding thermoforming process but uses the same principles as die forming. For the forming of sheet metal, such as automobile body parts, two parts may be used: one, called the punch, performs the stretching, bending, and/or blanking operation, while another part that is called the die block securely clamps the workpiece and provides similar stretching, bending, and/or blanking operation. The workpiece may pass through several stages using different tools or operations to obtain the final form. In the case of an automotive component there will usually be a shearing operation after the main forming is done and then additional crimping or rolling operations to ensure that all sharp edges are hidden and to add rigidity to the panel.

Die components
The main components for die tool sets are:
Die block – This is the main part that all the other parts are attached to.
Punch plate – This part holds and supports the different punches in place.
Blank punch – This part along with the blank die produces the blanked part.
Pierce punch – This part along with the pierce die removes parts from the blanked finished part.
Stripper plate – This is used to hold the material down on the blank/pierce die and strip the material off the punches.
Pilot – This will help to place the sheet accurately for the next stage of operation.
Guide, back gauge, or finger stop – These parts are all used to make sure that the material being worked on always goes in the same position, within the die, as the last one.
Setting (stop) block – This part is used to control the depth that the punch goes into the die.
Blanking dies – See blanking punch
Pierce die – See pierce punch.
Shank – used to hold in the presses. it should be aligned and situated at the center of gravity of the plate.